Description
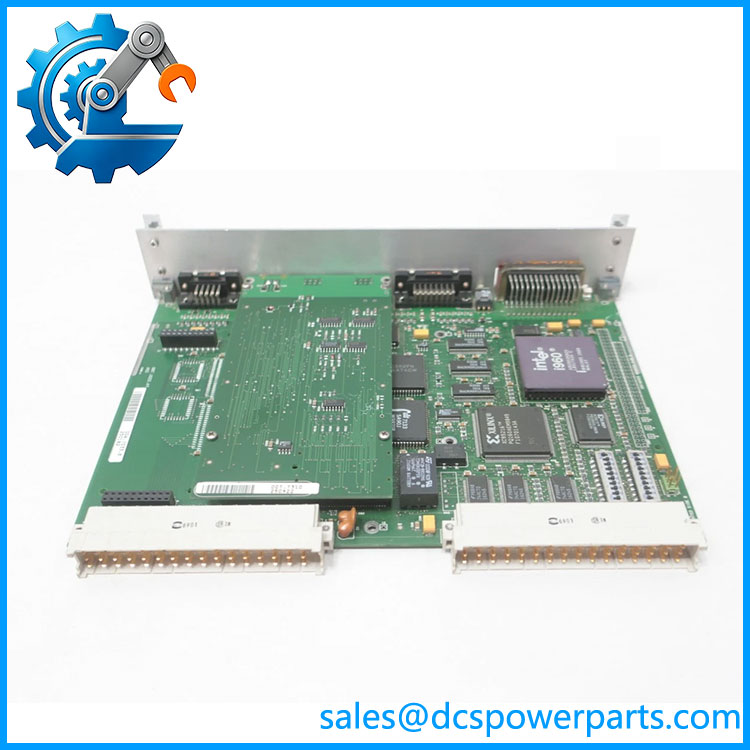
SOCAPEL PAM-R1N-H8F-AP-P V10800 H006.7538 Programmable Axis Manager
Product Introduction
The SOCAPEL PAM-R1N-H8F-AP-P V10800 is a legacy Programmable Axis Manager used in industrial motion-control systems. The PAM family belongs to the specialized motion-control side of the SOCAPEL product portfolio and should not be treated as a conventional PLC CPU or standard servo amplifier. Available equipment records identify the PAM-R1N-H8F-AP-P as a Programmable Axis Manager Controller with an 18–36 VDC supply range. The V10800 designation identifies a particular firmware or product revision within this legacy platform.
The controller’s purpose is to coordinate machine motion and manage programmable axis functions within a larger servo-control architecture. In practical terms, a PAM sits above the individual drive/power stages and provides machine-level motion coordination, sequencing and axis-management functions. This makes the unit relevant to CNC and other automated machinery where several servo axes must operate according to coordinated machine programs. Some secondary technical descriptions associate PAM equipment with trajectory processing, interpolation and electronic gearing, but those functions should be confirmed against the actual application configuration rather than assumed from the generic PAM family name.
For procurement, SOCAPEL PAM-R1N-H8F-AP-P V10800 should be ordered by the complete model and revision, not simply as a generic PAM controller. A current catalog identifies the V10900 version as a programmable axis manager with the same 18–36 VDC specification, while another exact-part listing identifies the V10800 unit as H006.7538. This revision distinction matters on older machines because the installed application, firmware behavior, drive interfaces and machine-specific parameters may depend on the exact PAM version.
Technical Specifications
| Specification | Details |
|---|---|
| Product Model | PAM-R1N-H8F-AP-P V10800 |
| Reference | H006.7538 |
| Manufacturer | SOCAPEL |
| Product Type | Programmable Axis Manager |
| Functional Category | Motion / servo control |
| Supply Voltage | 18–36 VDC |
| Nominal Supply | 24 VDC |
| Primary Function | Programmable axis management and coordinated motion control |
| Application | CNC and industrial machine motion systems |
| Controller Architecture | Stand-alone programmable motion controller |
| Programming / Configuration | Application-dependent legacy SOCAPEL motion-control environment |
| Communication | Exact interface configuration should be verified from the unit documentation |
| Feedback Interface | Exact configuration should be verified against the installed machine |
| Mounting | Application/cabinet dependent |
| Firmware Revision | V10800 |
| Lifecycle | Legacy / discontinued |
Specification caution: The 18–36 VDC supply and Programmable Axis Manager identification are supported by exact-part records. Detailed I/O, communication and encoder specifications should not be copied from unrelated PAM variants because the available online listings mix V10700, V10800 and V10900 revisions.
PAM-R1N-H8F-AP-P V10800
Main Features and Engineering Considerations
Dedicated Motion Management
The PAM architecture is intended for machine motion rather than general process automation. It provides a layer for coordinating programmable axes and machine sequences while dedicated servo hardware handles the motor power stage.
Multi-Axis Coordination
A Programmable Axis Manager is particularly useful where several axes must follow coordinated motion profiles. Depending on the original machine application, this can involve interpolation, electronic gearing, synchronization or programmed trajectories. The exact functions available on the installed configuration should be established from the machine application and original programming files.
Legacy Servo-System Integration
This controller is most valuable when maintaining an existing machine whose motion architecture was designed around SOCAPEL equipment. Replacing the PAM with a generic PLC or modern motion controller is not normally a simple hardware substitution. The machine program, axis scaling, servo tuning, homing behavior, limit handling and communication with the drives all need to be reproduced.
Firmware Revision Matters
The designation should remain part of the procurement description. Other PAM-R1N-H8F-AP-P records exist with V10700 and V10900 revisions. A catalog specifically lists V10900 as the same general Programmable Axis Manager reference, while another exact listing identifies . Do not assume that firmware revisions are interchangeable without confirming application compatibility.
18–36 VDC Supply
The controller is designed around a low-voltage DC control supply. The published range is 18–36 VDC. When replacing an installed unit, check the actual machine control power supply, fuse arrangement, grounding and voltage drop at the controller terminals rather than checking the nominal 24 VDC supply alone.
Application Program Is Critical
The hardware is only one part of a functioning PAM installation. Machine-specific motion programs, axis parameters and commissioning data may determine how the controller interacts with the servo system. Before removing an operating unit, preserve all available application files and parameter backups.
Application Scenarios
- CNC machine tools
- Multi-axis machine automation
- Coordinated servo systems
- Industrial positioning equipment
- Automated production machinery
- Legacy SOCAPEL motion-control systems
- Bosch Rexroth / Indramat-associated machine architectures
- Replacement of existing controllers
Engineer’s Guide: Field Pitfalls
1. Do not confuse the PAM with a servo drive.
The PAM is a motion-management/controller component. The servo amplifier or drive is responsible for the motor power stage.
2. Preserve the revision.
Do not substitute a V10700 or V10900 unit solely because the base model appears identical. Firmware and application compatibility must be checked.
3. Verify the complete reference.
For this unit, retain both and H006.7538 in purchasing records. Exact-part catalogs associate H006.7538 with this configuration.
4. Do not copy specifications from another PAM revision.
Online records contain mixed information for V10700, and V10900. Interface details should be confirmed from the actual hardware and machine documentation.
5. Back up the machine application before replacement.
A replacement controller without the original motion program and axis parameters may power up correctly but still fail to reproduce the machine’s operating sequence.
6. Check the servo-drive interface.
The PAM normally operates as part of a larger motion architecture. Verify how the installed PAM communicates with the associated drive amplifiers and feedback system before selecting a substitute.
7. Check the control power at the unit.
The published 18–36 VDC range does not eliminate the need to check voltage drop, grounding and transient behavior in the actual machine cabinet.
Frequently Asked Questions
What is SOCAPEL ?
It is a Programmable Axis Manager used in legacy industrial motion-control systems. Exact-part records identify it as a standalone motion-control device with an 18–36 VDC supply.
What is the H006.7538 reference?
is an associated reference for the configuration.
Is the a PLC?
Not in the conventional sense. It is a dedicated programmable motion/axis controller designed for coordinated machine motion.
What voltage does the use?
Available exact-part documentation identifies an 18–36 VDC supply range.
Is a firmware version?
It should be treated as a revision identifier associated with the particular PAM configuration. Records also exist for V10700 and , so the revision should be retained when sourcing a replacement.
Is the still a current product?
Available industrial-equipment records classify the as discontinued/legacy equipment. For an installed machine, repair or exact-replacement sourcing may therefore be preferable to assuming a modern controller is a direct replacement.
Procurement Note
For SOCAPEL .7538, the critical procurement information is the complete model, revision and associated .7538 reference. Confirm the installed controller against the machine documentation before accepting a V10700 or variant.
For an operating CNC or servo machine, request the original PAM application, axis parameters, drive configuration, feedback information and communication setup before replacing the hardware. The controller should be evaluated as one component of the complete motion-control architecture, not as an isolated 24 VDC electronic card.