Description
Product Features
The RH926KE is a high-density redundant I/O module launched by FOXBORO, specially designed for I/A Series distributed control systems. Optimized for high-reliability industrial process control scenarios, this module serves as a critical signal acquisition and data transmission bridge between field sensing equipment and DCS host systems. It integrates high-density signal processing, redundant fault-tolerant design and industrial anti-interference performance, effectively solving the problems of insufficient on-site signal access ports and poor system continuity. With outstanding operational stability, precise signal processing capability and flexible system adaptability, it ensures continuous and reliable operation of automated control systems in high-demand industrial production environments.
1. High-density Multi-channel Signal Processing: Adopting compact high-density circuit layout design, the module supports multi-channel synchronous signal acquisition and processing, which greatly improves the field signal access capacity of a single module. It can efficiently collect and sort various switching value and analog signals of on-site equipment, realizing centralized and refined management of field process signals and saving cabinet installation space.
2. Professional Redundant Fault-tolerant Architecture: Built with hardware-level redundant design for core circuits and signal channels. When a single channel or local circuit fails, the system can automatically switch to the backup channel without interruption of signal transmission and system operation. This fault-tolerant mechanism eliminates single-point failure risks of traditional I/O modules and significantly improves the overall reliability of industrial control systems.
3. High-precision Stable Signal Acquisition: Equipped with high-precision signal sampling chips and intelligent digital filtering algorithms. It can effectively filter industrial field clutter interference, voltage burrs and electromagnetic noise, ensuring low distortion and high repeatability of collected signals. The module maintains consistent signal accuracy under long-term continuous operation, meeting the high-precision monitoring and control requirements of process industries.
4. Strong System Compatibility & Expandability: Perfectly adapted to FOXBORO I/A Series DCS systems, supporting seamless bus docking and data interaction with system hosts, control modules and upper monitoring platforms. It supports flexible system capacity expansion and channel function configuration, which can meet the signal access requirements of different production scales and process links, with strong scene adaptability.
5. Industrial-grade Anti-interference & Environmental Resistance: Compliant with international industrial EMC electromagnetic compatibility standards, with built-in multi-stage shielding and surge suppression circuits. The whole machine adopts dust-proof, moisture-proof and anti-corrosion industrial protection technology, which can resist harsh environmental factors such as on-site high temperature, humidity, dust and strong electromagnetic interference, adapting to long-term industrial on-site operation.
6. Intelligent Self-diagnosis & Fault Alarm: Comes with built-in full-range operational self-diagnosis function. It real-timely monitors channel status, circuit operation, communication link and module temperature, automatically identifies abnormal signals, channel faults and communication failures, and outputs accurate alarm information and fault codes. It facilitates staff to quickly locate and eliminate faults and reduce system maintenance time.
7. Plug-and-play Modular Installation: Adopting standard industrial modular structure design, with unified installation dimensions and bus interface specifications. It supports fast plug-in installation and on-site replacement, no need for complex program debugging and wiring modification, effectively simplifying system construction and later maintenance work and improving engineering efficiency.
8. Long-term Continuous Operational Stability: Selects high-reliability industrial-grade electronic components, with optimized heat dissipation and power supply circuit design. It features low heat generation, low power consumption and ultra-low failure rate, supporting 24/7 long-term uninterrupted high-load operation, fully adapting to the continuous production mode of industrial process industries.
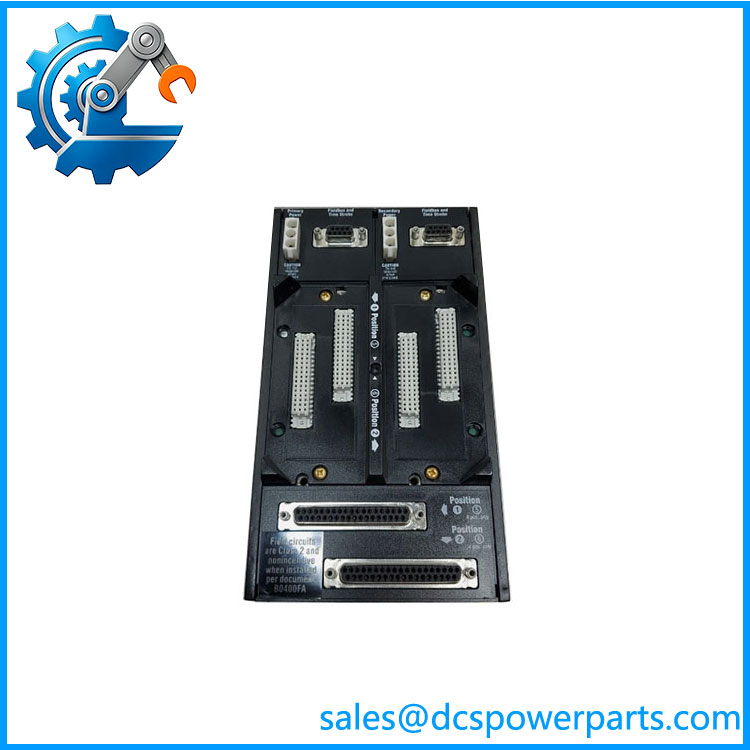
RH926KE
Product Parameters
|
Parameter Item
|
Technical Specification
|
|
Product Model
|
RH926KE
|
|
Brand
|
FOXBORO
|
|
Product Type
|
High-density Redundant Industrial I/O Module
|
|
Applicable System
|
FOXBORO I/A Series Distributed Control System
|
|
Core Function
|
Field signal acquisition, signal filtering processing, redundant signal transmission, system data interaction, real-time status diagnosis
|
|
Structural Feature
|
High-density channel design, hardware redundant fault-tolerant structure
|
|
Communication Mode
|
Dedicated DCS system bus communication
|
|
Signal Processing Performance
|
High sampling accuracy, low signal distortion, strong noise suppression capability
|
|
Anti-interference Standard
|
Compliant with industrial EMC electromagnetic compatibility certification
|
|
Diagnostic Function
|
Full-channel real-time self-diagnosis, fault alarm and operation log recording
|
|
Working Temperature
|
-20℃ ~ +70℃
|
|
Storage Temperature
|
-40℃ ~ +85℃
|
|
Working Humidity
|
5% – 95% RH (non-condensing)
|
|
Environmental Protection Grade
|
Industrial dustproof, moisture-proof and anti-corrosion grade
|
|
Installation Method
|
Standard cabinet rack plug-in installation
|
|
Continuous Operation Capacity
|
Support 24/7 long-term high-load stable operation
|
Product Usage Method
1. Pre-installation Inspection: Before installation, inspect the overall appearance, circuit board, interface terminals and golden fingers of the RH926KE module. Check for shell damage, interface wear, component looseness and circuit oxidation to ensure complete hardware integrity. Confirm that the module model matches the on-site FOXBORO I/A system to ensure effective compatibility.
2. On-site Static Protection: Complete the installation work in a dry, clean and ventilated industrial control cabinet. Wear professional anti-static gloves and anti-static wrist straps to avoid static electricity damaging the internal precision signal processing chips and redundant circuit structures of the module, ensuring safe and standardized construction.
3. Module Installation & Fixation: Align the module with the standard slot of the DCS system cabinet, insert it horizontally and smoothly, and lock the fixing buckle firmly. Ensure reliable contact between the module and the backplane bus to prevent poor contact, signal interruption and data deviation caused by long-term equipment vibration.
4. Standard Wiring Connection: Complete field signal wiring, system bus wiring and grounding wiring in strict accordance with FOXBORO official wiring specifications and industrial electrical safety standards. Classify and connect signal terminals, power terminals and communication terminals accurately to avoid wrong wiring, short circuit and signal crosstalk risks.
5. System Configuration & Debugging: After installation and wiring are completed correctly, connect the upper computer configuration software. Set channel parameters, signal acquisition modes, redundant switching logic and alarm threshold parameters according to on-site process control requirements, and download and save configuration files to complete system adaptation.
6. Power-on Test & Function Verification: Perform segmented power-on detection to activate the module’s self-diagnosis function. Observe the module status indicators to confirm normal power supply and stable communication link. Simulate field signal changes and single-channel fault conditions to verify signal acquisition accuracy and redundant switching reliability.
7. Daily Operation & Maintenance: After passing the function test, the module can be put into formal industrial operation. Regularly check the module operating temperature, terminal connection firmness and system operation logs, clean surface dust and heat dissipation channels regularly, and troubleshoot potential hidden dangers to ensure long-term stable operation of the DCS system.
Product Application Fields
1. Petrochemical Industry: Widely used in distributed control systems of oil exploitation, refining and chemical production devices. It is responsible for real-time acquisition and stable transmission of key process signals such as temperature, pressure, flow and liquid level of chemical reactors and production pipelines, ensuring accurate control and safe operation of chemical production processes.
2. Power Generation Industry: Applied in DCS control systems of thermal power, gas power and new energy power plants. It collects operating signals of core equipment such as generators, steam turbines and boilers, provides accurate data support for power generation process regulation and equipment safety monitoring, and improves the stability of power system operation.
3. Metallurgy & Heavy Industry: Suitable for automated control systems of metallurgical smelting, rolling and heavy machinery production lines. Adapting to harsh industrial environments with high dust, high temperature and strong vibration, it realizes long-term stable collection and transmission of production process signals, ensuring continuous and efficient operation of heavy industrial production lines.
4. Oil & Gas Storage and Transportation: Deployed in monitoring and control systems of long-distance oil and gas transmission pipelines, compression stations and storage bases. It supports unattended long-term monitoring operation, accurately feeds back pipeline operation status, and provides reliable data guarantee for safe transmission and intelligent scheduling of oil and gas resources.
5. Intelligent Process Manufacturing: Used in automated process control links of pharmaceutical, food processing and environmental protection industries. With high-precision signal processing and redundant fault-tolerant capabilities, it ensures the continuity and accuracy of process control, reduces production fluctuations and fault downtime, and improves the intelligent level of industrial production.