Description
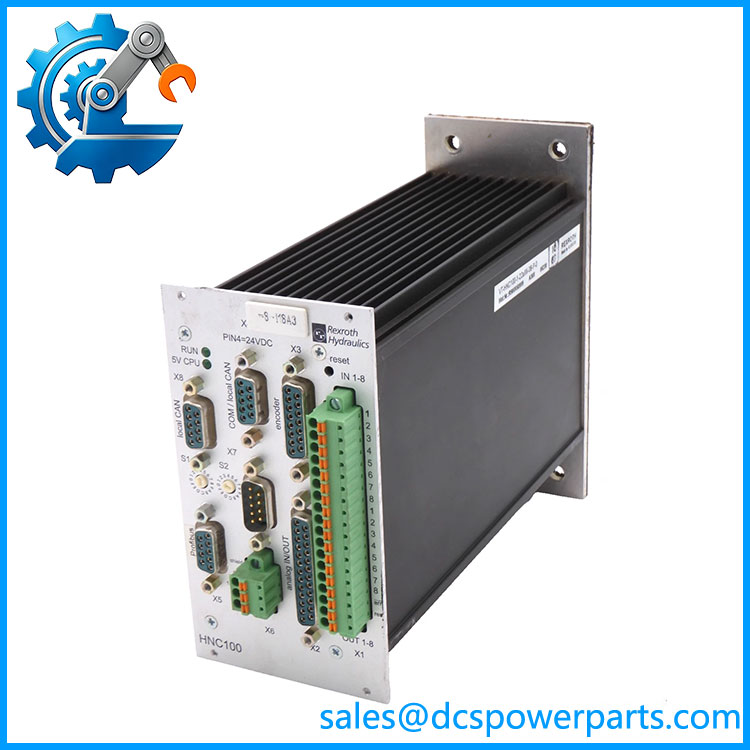
Bosch Rexroth SYHNC 100-NIB-23W-08-P-D-E23-A012 | Digital Axis Controller
Key Technical Specifications
| Parameter | Specification |
|---|---|
| Product Model | SYHNC 100-NIB-23W-08-P-D-E23-A012 |
| Manufacturer | Bosch Rexroth |
| Product Family | HNC100 / SYHNC 100 |
| Product Type | Digital Axis Controller / NC Controller |
| Controller Function | Programmable axis and hydraulic motion control |
| Supply Voltage | 24 VDC nominal |
| Permitted Supply | Approx. 17.5–30 VDC |
| Fieldbus | PROFIBUS DP |
| Digital Inputs | 8 |
| Digital Outputs | 8 |
| Analog Inputs | Configuration-dependent; documented family records include voltage/current inputs |
| Analog Outputs | Configuration-dependent; documented family records include voltage/current outputs |
| Measurement Interfaces | Configuration-dependent |
| Control Functions | Position, velocity, force/pressure, synchronous control |
| Programming | NC language / programmable motion control |
| Operating Temperature | Approximately 0 to +50°C in available records |
| Storage Temperature | Approximately -40 to +70°C |
| Relative Humidity | 10–95%, non-condensing, reported |
| Protection Rating | IP20, reported |
| Communication | PROFIBUS DP; other service/local interfaces depend on configuration |
| Exact Axis Count | Verify from the installed type code/manual |
| Exact Encoder Configuration | Verify from the installed hardware |
| Exact Current Consumption | Verify against the applicable hardware revision |
The P portion of the documented type code is associated with PROFIBUS communication, while the -08 configuration is associated in available technical records with eight digital inputs and eight digital outputs. Other measurement and analog interfaces are configuration-dependent, so they should not be inferred solely from the generic HNC100 family.
VT-HNC100-1-22/W-08-C-0
Product Introduction
The Bosch Rexroth SYHNC 100-NIB-23W-08-P-D-E23-A012 is a programmable digital axis controller from the HNC100 family. It is intended for applications where an industrial machine requires dedicated axis control rather than simply executing conventional PLC logic. Depending on the configured application, HNC100 controllers can handle position, velocity, force/pressure, and synchronized motion functions.
The controller is particularly relevant to hydraulic and electro-mechanical machinery where the control loop requires dedicated NC functionality and close coordination between feedback devices, valve or drive commands, machine sequencing, and a higher-level automation controller. The exact hardware configuration matters: the available records identify PROFIBUS and the -08 I/O configuration, but do not provide enough authoritative evidence to treat every analog, encoder, and axis interface as universal to this exact suffix.
Engineering Pain Point
The biggest replacement risk is treating SYHNC 100-NIB-23W-08-P-D-E23-A012 as an ordinary PLC CPU. It is part of a motion-control architecture, so the controller’s stored NC program, axis parameters, feedback scaling, control-loop parameters, I/O assignment, and PROFIBUS configuration can all affect machine behavior. A replacement that powers up and communicates with the PLC can still be incorrectly configured for the hydraulic or mechanical system.
Typical Applications
- Hydraulic axis control: Position, velocity, and pressure-related control of hydraulic cylinders and actuators.
- Machine tools: Dedicated NC axis control where motion behavior is handled separately from higher-level PLC sequencing.
- Press and forming equipment: Coordinated movement and force/position control of hydraulic machinery.
- Special-purpose machinery: Programmable axis control integrated with a supervisory PLC or industrial fieldbus.
Technical Pitfalls to Avoid
- Verify the complete type code.
The long suffix is not cosmetic. Interface and I/O configuration are encoded through the HNC100 ordering structure. Do not substitute another HNC100 unit merely because its enclosure and connector arrangement look similar. - Back up the NC program and machine parameters.
The controller’s application is part of the machine’s motion behavior. Preserve the original NC program, axis parameters, calibration values, and commissioning data before removing a functioning controller. - Check PROFIBUS configuration separately.
ThePconfiguration identifies PROFIBUS capability in the available records. The PLC project must still contain the correct device configuration, address, process-data mapping, and diagnostic handling. - Do not assume every has the same feedback interfaces.
Available secondary records describe combinations of incremental, SSI, 1 Vpp, EnDat, analog, and other measurement interfaces. The exact installed hardware should determine what can actually be connected. - Verify the hydraulic control loop before commissioning.
Valve command scaling, pressure feedback, position feedback, direction, enable logic, and limit handling should be checked before allowing full-speed or full-force machine movement. - Check the 24 VDC supply under load.
A nominally correct supply voltage does not guarantee correct operation. Measure the supply at the controller during machine switching and valve/actuator operation, particularly in older cabinets with long DC wiring. - Do not infer eight controlled axes from the
-08designation.
Available listings describe-08as an 8-channel I/O configuration, while other records describe variants by axis capability. The number of I/O channels and the number of controlled axes are separate parameters.
Related Products
- Bosch Rexroth — The broader digital NC/digital axis controller family to which this SYHNC 100 unit belongs.
- Bosch Rexroth SYHNC 100-NIB-23/W-04-P-D-E23-A012 — Related configuration reported with a different I/O count; verify the complete type code before substitution.
- Bosch Rexroth VT-HACD — Hydraulic control electronics family used for dedicated hydraulic valve control; it is not automatically equivalent to an controller.
- Bosch Rexroth VT-VSPD-1 — Digital proportional-valve amplifier family; performs valve amplification rather than replacing the ‘s axis-control role.
- Bosch Rexroth IndraControl / IndraLogic controllers — Higher-level control products that may participate in Rexroth automation architectures, but they should not be treated as direct replacements without reviewing the machine architecture.
- PROFIBUS DP interface — The fieldbus connection associated with the
Pconfiguration; PLC-side configuration must match the installed controller. - Rexroth hydraulic servo/proportional valves — Field actuators that may be controlled through the architecture; the valve’s command range and feedback arrangement must match the controller configuration.
Procurement and Replacement Note
For SYHNC 100-NIB-23W-08-P-D-E23-A012, procurement should capture the complete type code, hardware revision, installed NC software/program, axis parameters, PROFIBUS configuration, I/O wiring, feedback type, and machine-specific calibration data.
I would not approve a replacement solely from the description “ digital axis controller.” The exact suffix identifies a configured hardware variant, while the machine’s stored software and parameters determine how that hardware behaves in the actual motion-control application. Available public records also contain conflicting claims about the exact axis count and detailed measurement interfaces for this particular suffix, so those values should be verified from the controller nameplate, original Rexroth documentation, or the installed machine drawings before engineering a substitution.